

A Long-Term Partner Supporting Brands from Concept to Growth
Since its establishment in 2002, Blackbird has focused on skincare formulation development and manufacturing, providing Private Label and Custom Development solutions for skincare brands.
We go beyond manufacturing by helping brands make informed decisions before production begins. From product concept and formula development to market launch and ongoing growth, we work as an extension of your team, supporting you throughout the entire journey.
Why Blackbird
Beyond Manufacturing
01 Market Insights
Through market research, beauty exhibitions, and channel insights, we identify consumer needs and category trends to guide product development.
02 Trend-to-Product Development
We turn market trends, ingredient innovations, and product opportunities into practical product directions.
03 Brand Growth Support
From first products to product expansion and scaled production, we provide support tailored to each growth stage.
04 Close Brand Collaboration
We work closely with brands to understand their goals and solve challenges throughout the development process.
05 Flexible Development Support
We optimize formulas, textures, packaging, and costs to create solutions that fit market and business needs.
06 Global Market Support
We support testing, regulatory documentation, packaging requirements, and market preparation for US and European markets.
R&D Capability

How Our Laboratory Supports Product Development
We do not move formulas directly into production without evaluation. Before scaling up manufacturing, our R&D and quality teams assess formula feasibility, ingredient compliance, stability risks, packaging compatibility, and production readiness — helping brands reduce development risks before product launch.
Product Requirement Analysis
We first understand the product objectives:
- Product positioning
- Functional requirements
- Sensory experience
- Target price
- Packaging requirements
- MOQ requirements
Based on brand needs, we develop suitable product development directions.
Formula & Packaging Evaluation
The R&D team evaluates:
- Formula system
- Ingredient selection
- Sensory performance
- Packaging compatibility
- Cost feasibility
Ensuring the product solution meets development goals and has a solid foundation for manufacturing.
Sample Development & Optimization
Starting from laboratory samples:
- Formula adjustments
- Performance optimization
- Sensory experience optimization
- Stability observation
Through multiple rounds of testing and refinement, we help products achieve the expected performance.
Testing & Validation
Before mass production, we conduct:
- Efficacy testing
- Stability testing
- Packaging compatibility testing
- Product safety evaluation
Relevant testing reports are provided to support product launch.
Scale-Up Evaluation & Mass Production Confirmation
The R&D and production teams jointly evaluate:
- Manufacturing process feasibility
- Equipment compatibility
- Batch production stability
Ensuring laboratory samples can be successfully transferred into stable large-scale production.
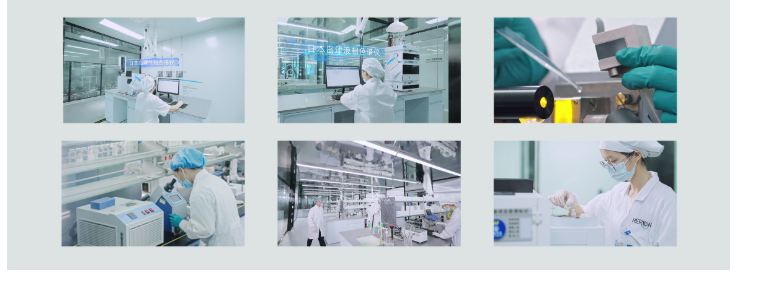
Laboratory Testing Capabilities
Raw Material Testing
Compares incoming materials with agreed identity and specifications. The record should identify the material, batch, specification and result.

Physical & Chemical Testing
Checks the agreed physical and chemical properties of the sample. Review the measurement, method and acceptance range together.
Efficacy Testing
Assesses selected product claims under defined conditions. The report should identify the formula, method, outcome and limitations.

Safety Testing
Evaluates safety questions relevant to the product and its intended use. Review the assessed sample, evaluation scope and conclusion.
Stability Testing
Evaluates changes in the formula over time under defined storage conditions. Review the formula, packaging, duration, conditions and observations together.
Microbiological Testing
Checks the sample against the microbiological limits specified for the product. The record should identify the sample or batch, test method, limits and result.
Raw Material Supply System
Stable Raw Material Resources Supporting Continuous Product Development
Blackbird maintains stable partnerships with long-term raw material suppliers and continuously monitors global ingredient trends, helping brands access reliable ingredient options and more suitable formulation solutions.
Support:
- Stable raw material supply
- Global ingredient trend tracking
- Exploration of innovative ingredient applications
- Formulation development resources support

Manufacturing Capability
- 25,000㎡Manufacturing Facility
- 2,000㎡Class 100,000 Clean Production Workshop
- 15Production and filling lines
- GMP &
ISO 22716Manufacturing Standards


Advanced Equipment & Manufacturing Systems
Supporting Different Product Types and Production Scales


- Various German Technology Vacuum Homogenizing & Emulsifying Equipment
- Automatic Filling Machines
- Automatic Sealing Machines
- EDI Pure Water System
Daily Production Capacity
Supporting flexible production from initial batches to large-scale orders.
| Product Type | Daily Output | Capacity |
|---|---|---|
| Creams & Lotions | 100,000units/day | |
| Toners & Serums | 200,000units/day | |
| Sheet Masks | 150,000boxes/day (4 sheets per box) | |
| Product Sets | 50,000sets/day |
Full-Process
Quality Control
Blackbird integrates quality control across the entire product lifecycle to ensure stable production and support long-term repeat orders.
Final Product Confirmation
Ensuring products meet approved standards
- Formula and packaging confirmation
- Final sample testing
- Shipping and transportation simulation
- Packaging quality inspection

Pre-Production Control
Ensuring production readiness
- Raw material and packaging confirmation
- Production order confirmation
- Material preparation
- Bulk testing
Production Stability & Control
Ensuring batch consistency
- First article inspection on filling lines
- Mass production execution
- In-process sampling inspection
- Non-conforming product management

Delivery & Ongoing Monitoring
Supporting consistent quality and supply
- Shipment preparation and quantity verification
- Finished product storage management
- Continuous quality monitoring
- Batch traceability management
Global Quality Standards
Blackbird maintains manufacturing systems and quality capabilities that support requirements across the US, EU, UK, and other global markets.
- ISO 9001
- ISO 22716
- GMPC
- FDA
- CPSR
- FSC
- EPR
- Intertek-
recognized - AQL Level II
Build Your Next Skincare Product With Blackbird
Whether you are developing a hero product, expanding your skincare line, preparing for retail, or scaling repeat production, Blackbird can support your next stage of growth.